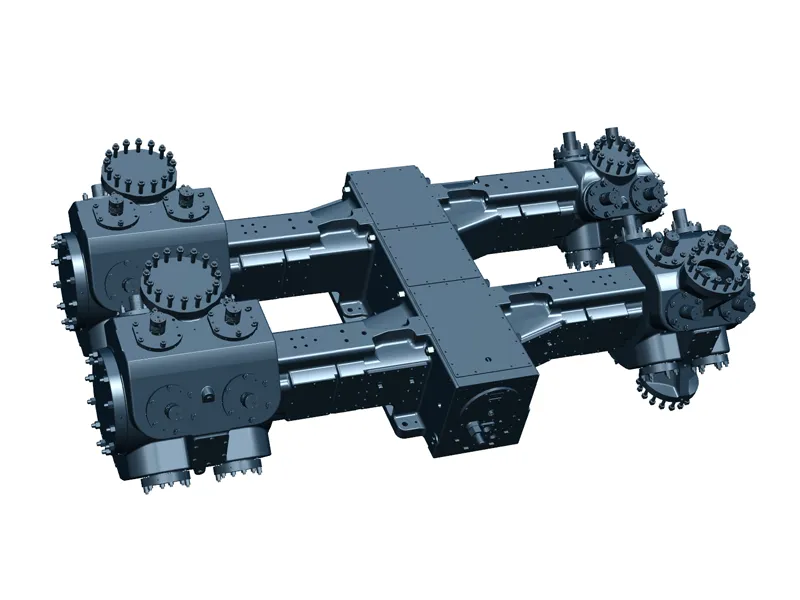
Reciprocating compressor valves are small components with an outsized influence on machine performance. They open and close in response to pressure differences across the valve element, allowing gas to enter a cylinder during suction and leave it during discharge. When a valve does not move freely or seal as intended, the cylinder may no longer deliver the expected mass flow, and the compressor can experience higher temperatures, reduced capacity or an increase in power demand.
A valve problem should not be diagnosed from one symptom alone. Similar operating signs can result from changes in gas composition, cylinder conditions, cooling, instrumentation or other mechanical issues. A useful investigation connects operating history with inspection findings and the specific duty of the machine.
How Suction and Discharge Valves Work
In a reciprocating compressor, piston movement changes cylinder volume and pressure. During the suction portion of the cycle, cylinder pressure falls below the suction-side pressure and the suction valve opens. As the piston moves through compression, cylinder pressure rises. Once it exceeds the discharge-side pressure by the amount required to open the discharge valve, gas flows into the discharge system.
The valves are commonly automatic: pressure differences, rather than a separate actuator, drive their opening and closing. The valve element, seat, spring or lift limiter must respond to repeated cycles while maintaining an effective seal when closed. Exact construction varies by valve design and service.
A valve that leaks or responds slowly affects the pressure-volume process inside the cylinder. Gas may flow back across a valve instead of moving through the intended path. The compressor can then do extra work without delivering the expected output. This is why valve condition matters not only for maintenance cost, but also for capacity, temperature and operating stability.
How Operating Conditions Affect Valve Loading
Valve life is influenced by the gas being compressed and by the way the machine is operated. Pressure ratio, suction conditions, discharge pressure, gas properties and cycle frequency all contribute to the mechanical and thermal duty experienced by the valve. A change in process conditions can therefore alter valve behavior even when the compressor itself has not been modified.
Higher cycle frequency means the valve element repeats its movement more often. Depending on the design and duty, this can increase the importance of impact, fatigue and dynamic response. Pressure differences influence how the valve opens and closes; abnormal pressure conditions or a mismatch between the valve and its operating range may contribute to poor sealing or excessive movement.
Temperature also matters. Hotter gas can affect material properties, clearances and the thermal environment around the valve. The source of a temperature change should be established before attributing it to valve failure: high discharge temperature may relate to compression conditions, cooling performance, leakage, or several factors together.
Gas composition and contaminants require particular attention. Corrosive constituents may attack materials; particles can interfere with sealing surfaces; deposits can restrict movement; and liquids entering a cylinder can create abnormal loading. These are different mechanisms and should not be grouped into a single generic diagnosis. The appropriate response depends on the gas specification, the valve construction and the evidence found during inspection.
Contamination and Liquid Carryover: Different Risks
Particles and deposits can prevent the valve element from seating consistently. The resulting leakage may reduce volumetric efficiency and increase local heating. Abrasive material can also damage contact surfaces, while corrosive components may degrade parts over time. Filters, upstream separation and process cleanliness should therefore be reviewed alongside the valve itself.
Liquid carryover presents a separate concern. Reciprocating compressors are designed for a specified gas service, and liquid entering a cylinder can change the load on internal components. Depending on the amount, location and operating conditions, liquid may damage valve parts or other cylinder components. The presence of liquid should prompt a review of upstream separation, drains, process upsets and the effectiveness of interstage equipment where applicable.
Finding contamination in a valve does not automatically identify where it originated. Inspection should record the type and distribution of deposits or damage, then compare those observations with gas data, filter condition, separator operation and recent process changes. This helps distinguish a local component issue from a system-level cause that could damage a replacement valve as well.
Recognizing Valve Problems During Operation
No single indicator proves a valve has failed, but several changes can justify investigation. These include a decline in delivered capacity, unusual cylinder or discharge temperatures, a change in power demand, unexpected pressure behavior, abnormal noise, or a change in the time required to reach operating conditions. The significance of each signal depends on the compressor design and the baseline established for that machine.
Trends are more informative than isolated readings. Compare current data with previous operation at similar suction pressure, discharge pressure, gas composition and load. Confirm instrument accuracy and check whether process demand or control settings have changed. If one cylinder behaves differently from comparable cylinders, that difference may help narrow the investigation, but it is not a substitute for inspection.
A disciplined diagnostic sequence is useful: verify the operating point; review recent process events; compare temperature, pressure and capacity trends; check relevant upstream equipment; and inspect the valve when the operating evidence supports doing so. Follow the manufacturer's procedures and site safety requirements before opening equipment. Valve removal and examination should be carried out only after isolation, depressurization and other required safeguards.
How Valve Design and Maintenance Decisions Affect Reliability
Valve selection should match the gas service, pressure conditions, temperature range, speed and compressor design. A component suitable for one duty should not be assumed suitable for another simply because the connection dimensions are similar. Material compatibility, expected contamination, maintenance access and the manufacturer's limits should be reviewed together.
Inspection should look for damaged or distorted valve elements, worn seating surfaces, deposits, corrosion, broken or weakened springs where fitted, and evidence of abnormal contact. The inspection record should identify the location and condition of each part rather than only stating that the valve was “worn.” Photographs and comparisons with the applicable drawing or service guidance can help the engineering team assess the findings.
Replacing damaged parts may restore the intended sealing function, but recurring failure calls for a broader review. If a replacement valve fails again soon after service, investigate whether the root cause remains: operating conditions may have changed, contamination may still be present, or the selected design may not suit the actual duty. Maintenance intervals should be informed by manufacturer guidance, operating history and inspection evidence, not by a universal interval applied to every machine.
For operators reviewing a reciprocating gas compressor, valve symptoms should be assessed in the context of the complete process and cylinder duty. Where inspection indicates that repair, replacement or a wider machine review may be needed, QualRotate's reciprocating compressor repair service page provides the relevant route to discuss parts and maintenance support. The product range can also be reviewed on the reciprocating compressors page.
Frequently Asked Questions
What are the common signs of a reciprocating compressor valve problem?
Possible signs include reduced capacity, abnormal temperature, changes in power demand, unusual noise or unexpected pressure behavior. None is conclusive on its own; confirm the operating point, instrumentation and inspection evidence before identifying the cause.
What causes compressor valves to fail?
Potential causes include repeated cyclic loading, unsuitable operating conditions, wear, contamination, corrosion, deposits or liquid carryover. The dominant mechanism depends on valve design and the gas service.
Can a leaking valve increase discharge temperature?
It can contribute to abnormal heating because gas may leak back and be recompressed, but discharge temperature also depends on pressure ratio, suction temperature, cooling and other conditions. A diagnosis should consider these factors together.
How often should reciprocating compressor valves be inspected?
There is no single interval suitable for every compressor. Use the manufacturer's recommendations, service severity, operating history and inspection findings to establish an appropriate maintenance plan.
Should a valve be replaced whenever capacity falls?
Not automatically. Capacity loss can have several causes. Check operating conditions, instrumentation and other relevant systems, then inspect the valve when the evidence points to a valve-related issue.
Can liquid entering the cylinder damage a valve?
Liquid carryover can create abnormal loading and may damage valve or cylinder components. The event should also trigger a review of upstream separation and process conditions to reduce the risk of repeat damage.
 English
 中文